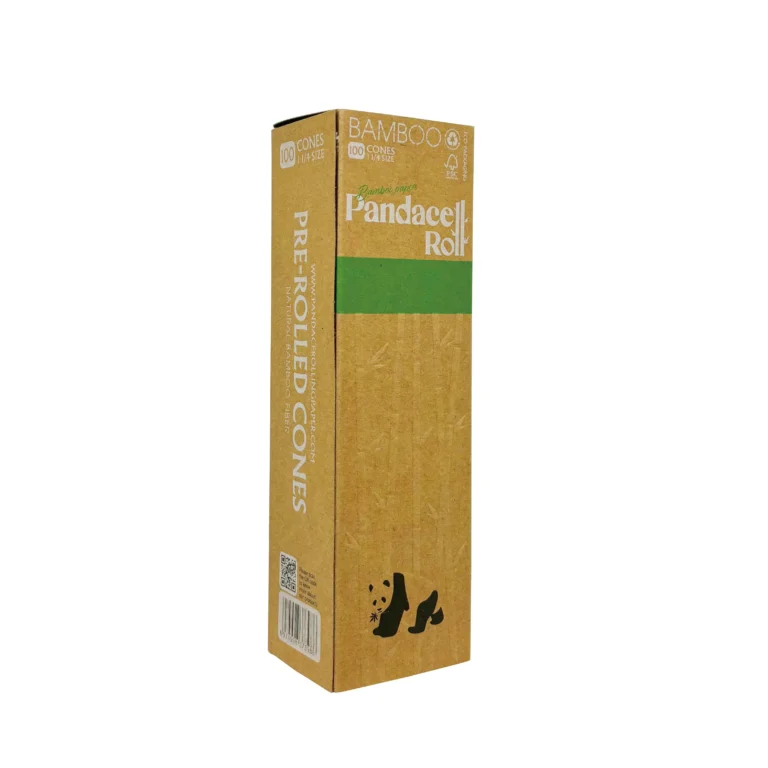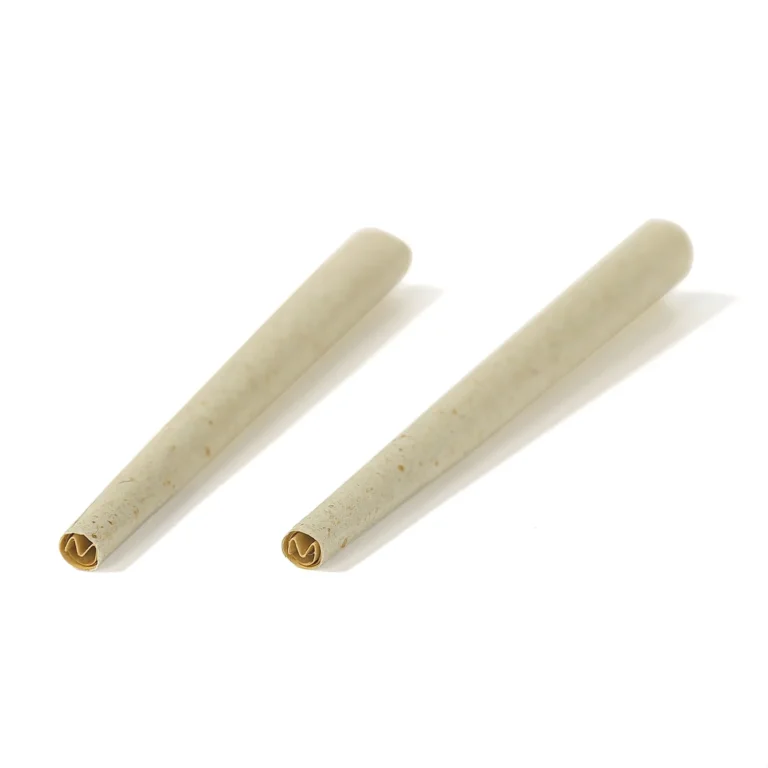

For commercial pre-roll processors and packaging facilities, operating high-speed automated filling machinery requires paper supplies that can withstand continuous mechanical stress. When using vibration-based packing tables, choosing paper cones with inadequate physical properties leads to split seams, crumpled tips, and machine jams.
To optimize production line efficiency, brands must source Knockbox pre-roll cones MD/CD tensile strength parameters that comply with rigorous ISO paper testing standards. Sourcing cones engineered with a balanced Machine Direction (MD) and Cross Direction (CD) tensile ratio ensures that the paper sheets can absorb high-frequency vibrations without tearing, keeping production line defect rates under 0.01%.
Understanding the mechanics of vibration-based filling, ISO 1924 tensile testing standards, and paper fiber alignment technologies will help you audit suppliers and protect your manufacturing margins.
—
How does automated filling impact pre-rolled cone structural integrity?
Industrial packing machines, such as the Futurola Knockbox series (including Knockbox 100, 300, and 500 models), process multiple cone sizes concurrently. These include standard 1 1/4 size (84mm length with a 26mm tip), 98 Special (98mm/26mm), and King Size (109mm/21mm or 109mm/26mm).
During the 60-to-90-second packing cycle, the machine subjects the paper cones to rapid vertical oscillations. This physical force consolidates the herbal material inside the cone, eliminating air pockets:
- Vertical Impact Stress: The downward force of the herb column exerts axial pressure along the length of the cone, testing the stiffness of the paperboard tip.
- Radial Expansion Tension: As the material compacts, it exerts outward radial force against the paper wall. This radial expansion puts direct tension on the paper’s glue line and seams.
- Vibrational Fatigue: High-frequency vibrations test the micro-bonding structure of the plant fibers, making weak paper prone to sudden tears.
—
What do ISO 1924 standards reveal about paper tensile parameters?
In paper engineering, tensile strength is measured using the ISO 1924-1 and ISO 1924-2 standards, which define the force required to break a paper strip of a specific width under a constant rate of elongation.
For specialty thin papers (12 GSM to 20 GSM) used in pre-roll manufacturing, the directional alignment of the paper fibers determines its mechanical behavior:
- Machine Direction (MD) Tensile Strength: The strength along the direction the paper web moved on the paper-making machine. For machine-ready bobbins, MD tensile strength should exceed 1.5 kN/m (and up to 1.9 kN/m for high-volume lines).
- Cross Direction (CD) Tensile Strength: The strength perpendicular to the machine flow. Because paper fibers naturally align longitudinally, CD strength is typically lower.
- The MD/CD Ratio: Standard papers have an MD/CD ratio of 2:1 or 3:1. However, since automated filling exerts radial (CD) expansion forces, a high MD/CD anisotropy leads to splitting along the longitudinal seams.
| Paper Material | Base GSM Weight | Required MD Tensile | Required CD Tensile | Target MD/CD Ratio |
|---|---|---|---|---|
| High-Tensile Rice | 12 GSM – 13 GSM | ≥ 1.5 kN/m | ≥ 0.9 kN/m | 1.6 : 1 |
| Organic Hemp | 13 GSM – 14 GSM | ≥ 1.6 kN/m | ≥ 1.0 kN/m | 1.6 : 1 |
| Refined Wood Pulp | 14 GSM – 18 GSM | ≥ 1.8 kN/m | ≥ 1.1 kN/m | 1.5 : 1 |
—
How do advanced paper-making processes optimize the MD/CD ratio?
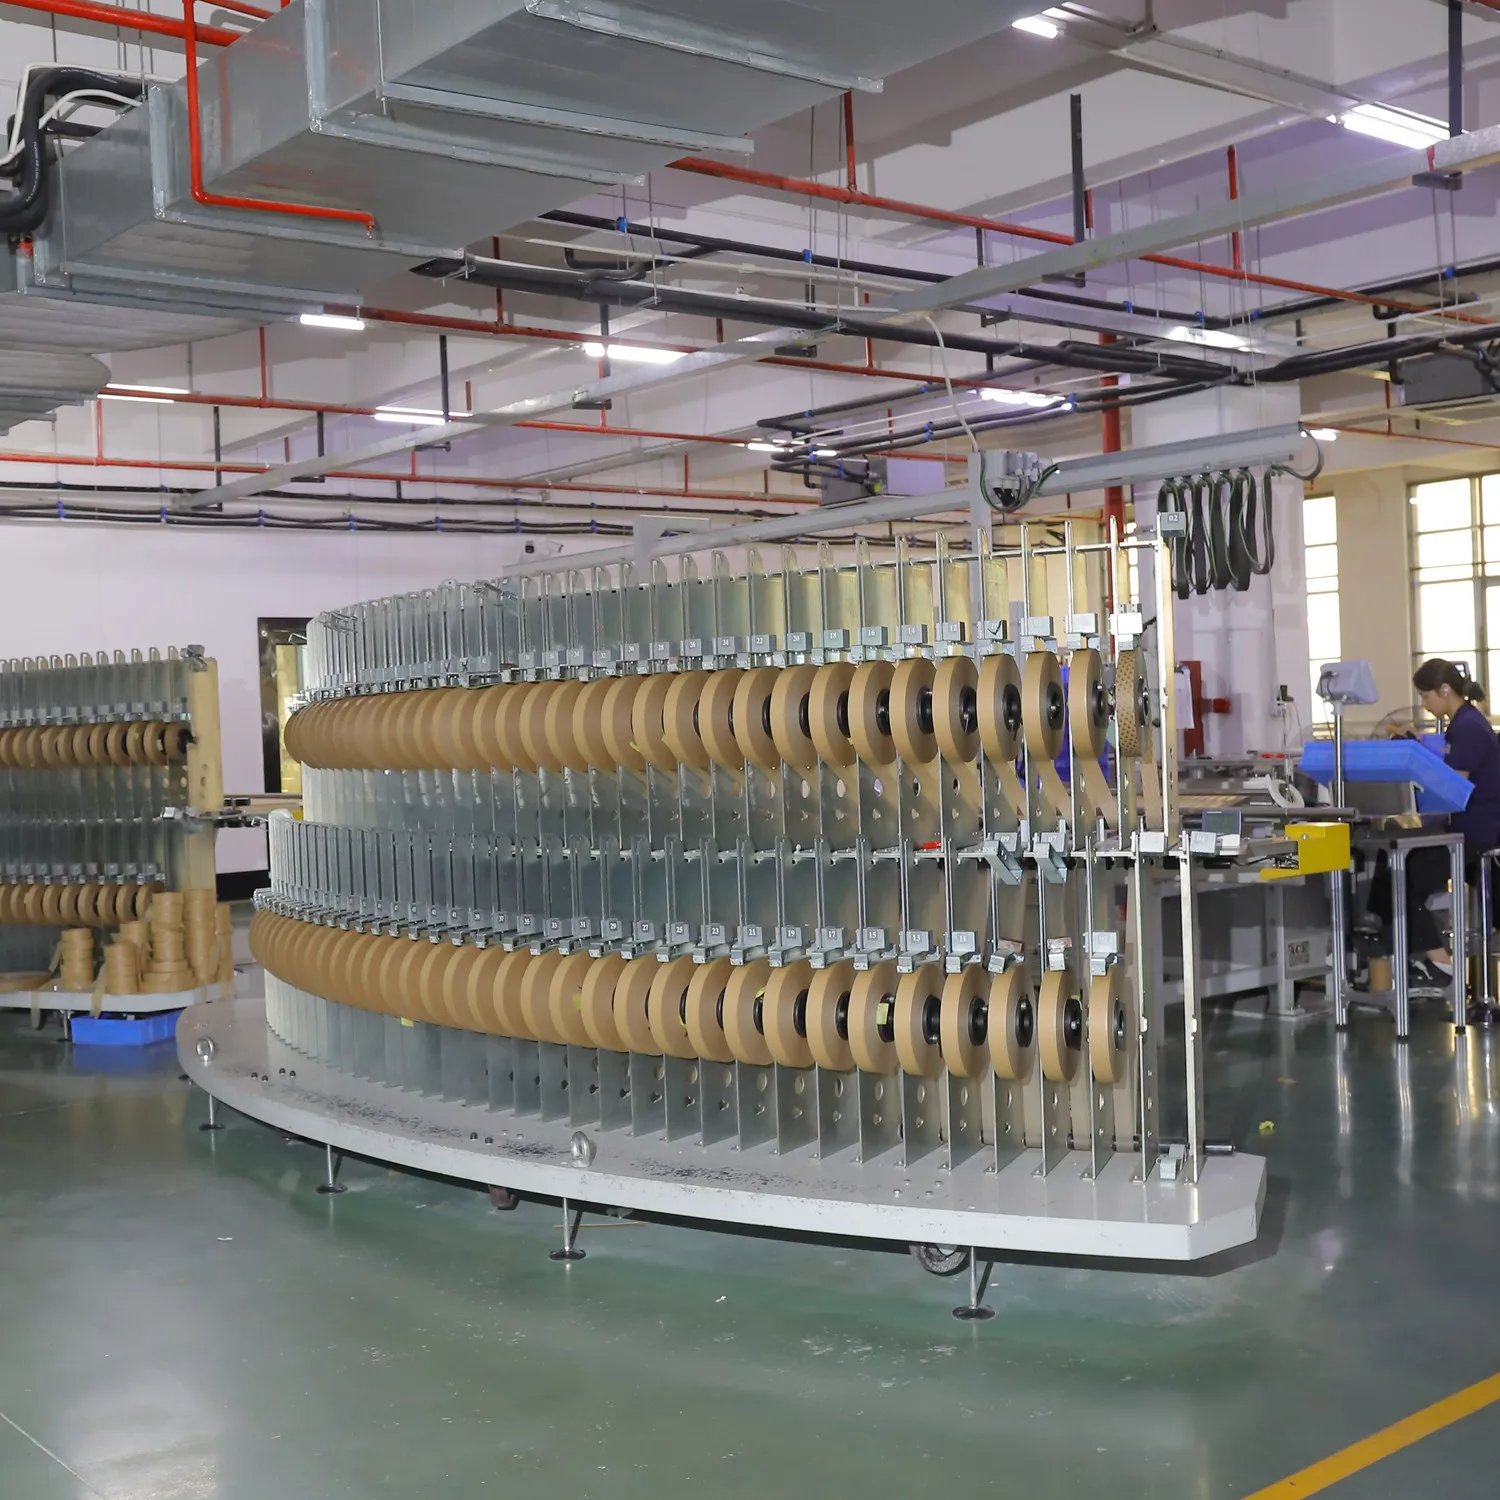
To prevent splitting on the Knockbox table, direct manufacturers utilize advanced headbox (流浆箱) and slice geometry control to randomize fiber orientation during the wet-end forming phase.
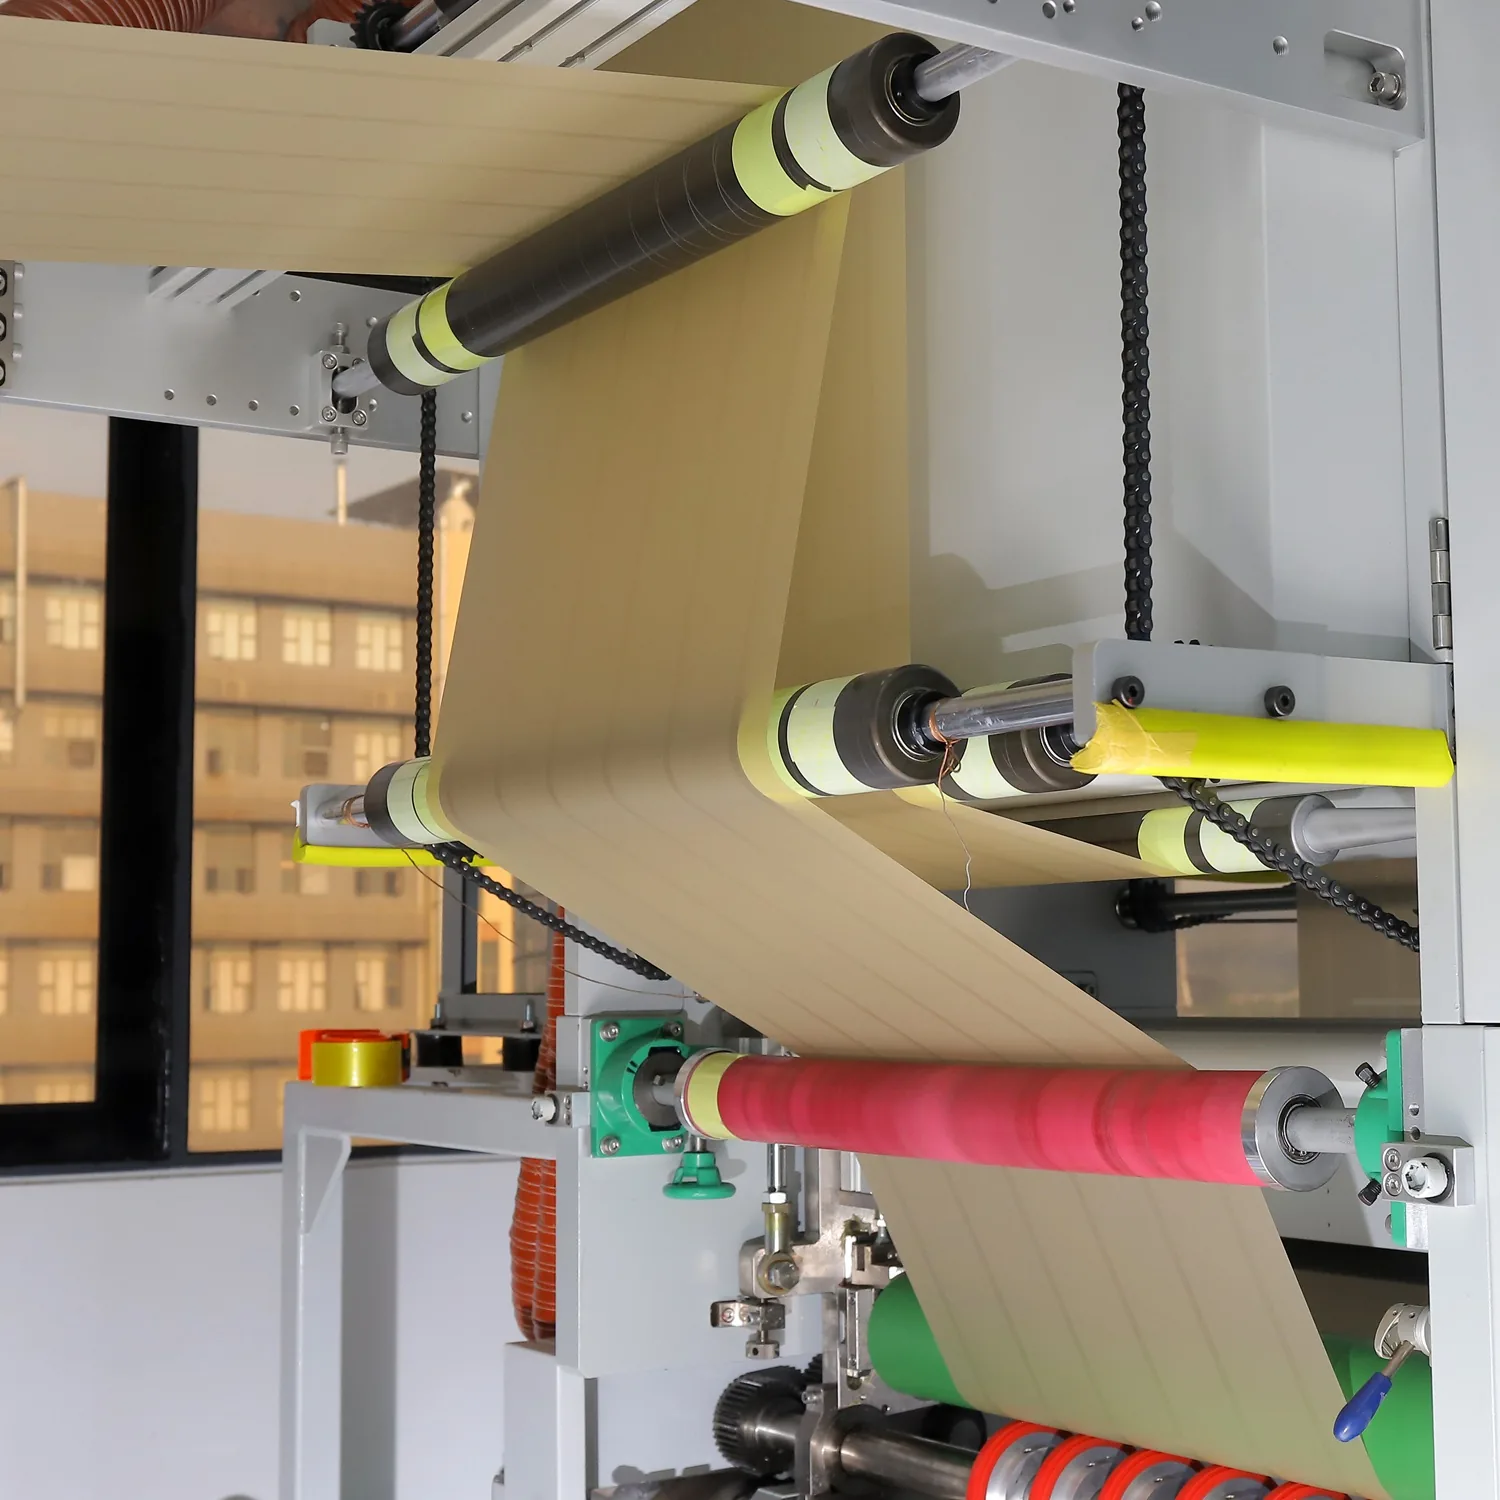
Our manufacturing facility optimizes paper runnability through:
- Turbulence Control: Generating controlled micro-turbulence in the headbox to prevent fibers from grouping together and aligning solely in the machine direction.
- Jet-to-Wire Speed Adjustment: Matching the slurry jet speed to the wire speed to randomize fiber layout, bringing the MD/CD ratio closer to a balanced 1.5:1 configuration.
- Precision Slitting: Utilizing high-accuracy circular blades to slice paper rolls cleanly without creating micro-tears along the edges, which would act as stress concentration points during winding.
Sourcing Checklist for Automated Pre-Roll Filling
- [ ] Confirm your pre-rolled cones are compatible with the specific tray molds of your Knockbox model.
- [ ] Request the ISO 1924 tensile test sheets (detailing MD and CD values) from the factory lab.
- [ ] Verify that the paper sheets have an MD/CD anisotropy ratio of 1.6:1 or lower.
- [ ] Test a sample batch of 1,000 cones at full machine packing speed to verify a splitting rate under 0.01%.