
I’ve had a buyer send me a canoeing complaint that had nothing to do with rolling technique. The seam was the actual problem.
Check seam integrity at three points: a visual inspection pass for gum coverage and gaps, an interval-based physical adhesion test throughout the production run, and a handling/transit simulation on a sample carton—skip any one and defects can slip through to a shipped batch.
Read this and you’ll know exactly where in your QC process seam failure actually gets caught, instead of only finding out from a customer complaint.
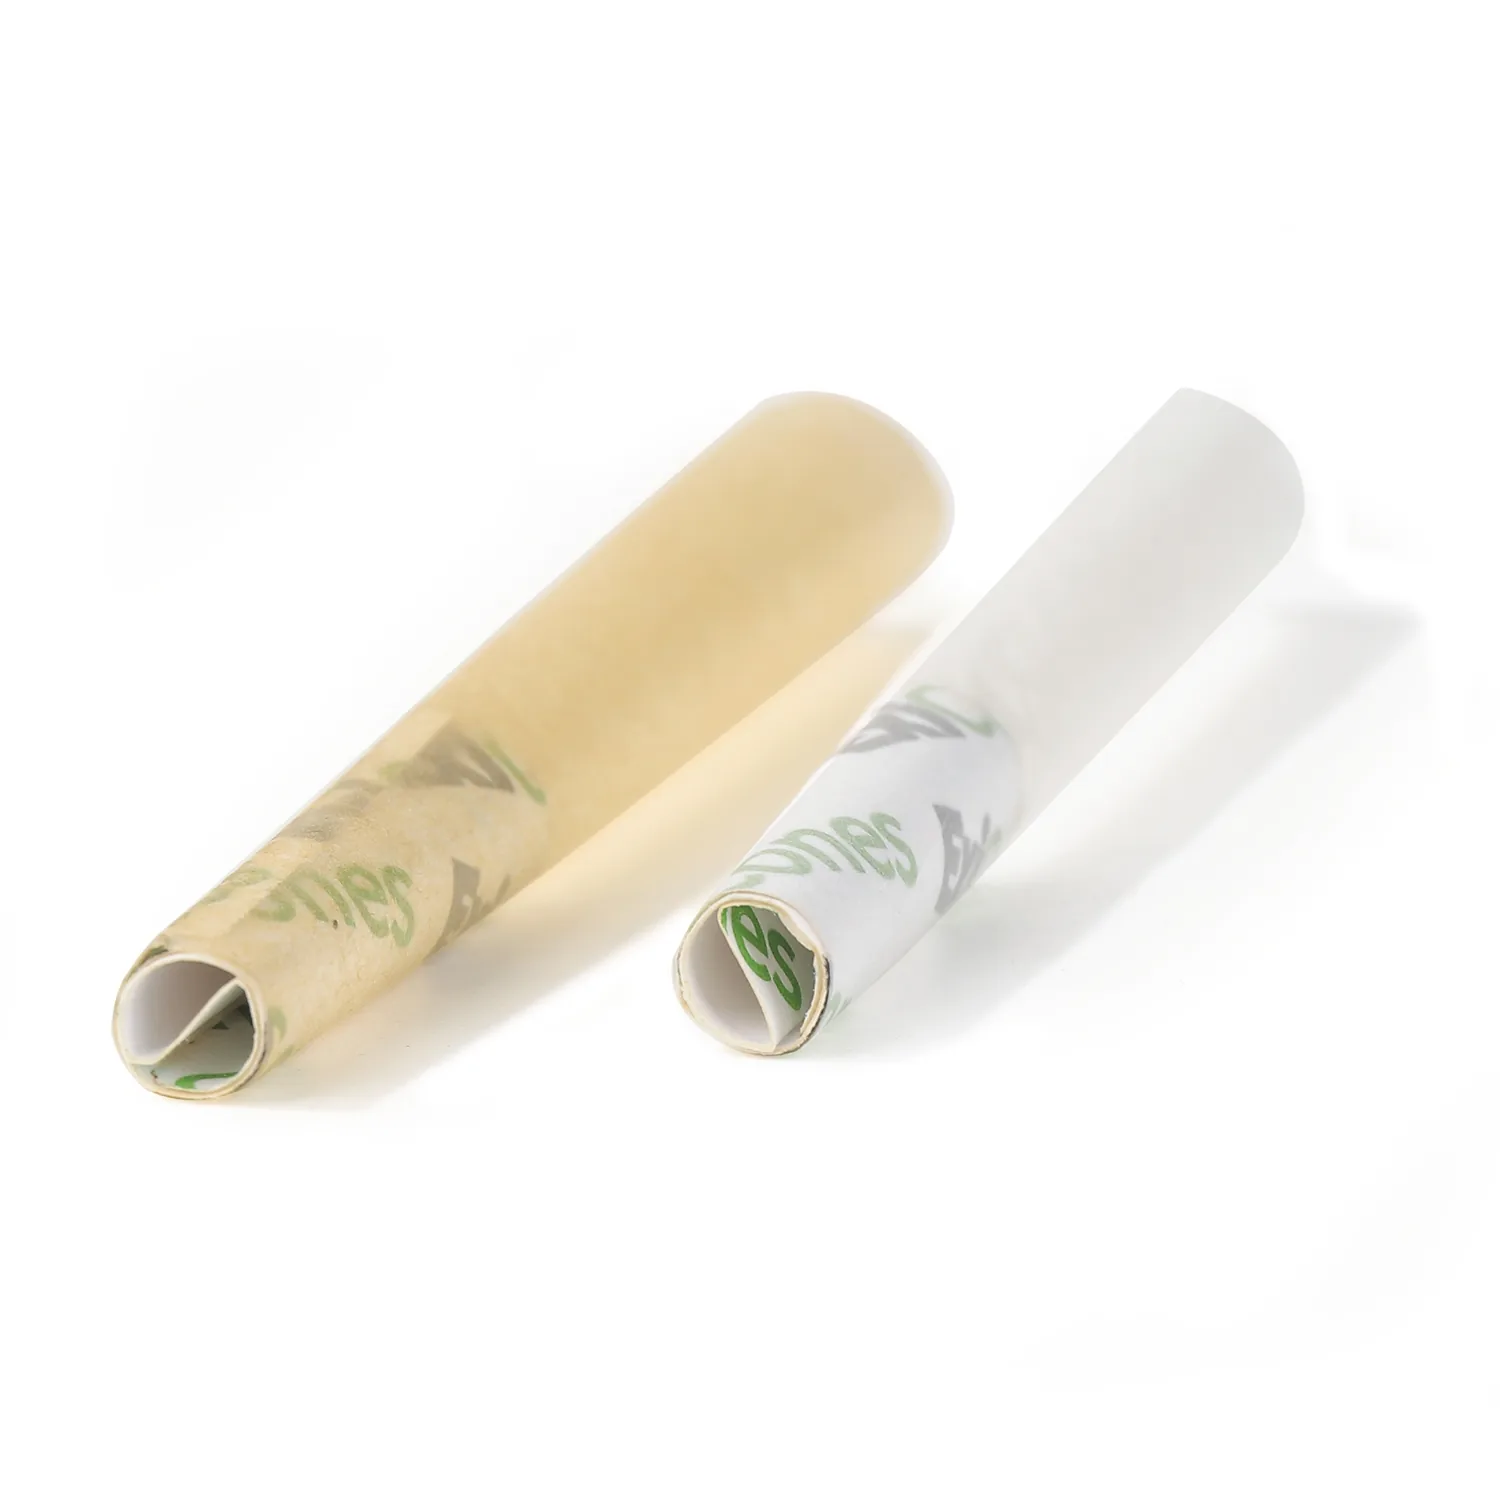
What Actually Causes a Cone Seam to Fail in the First Place?
I hear “the paper was bad” a lot. It’s rarely that simple.
Seam failure usually traces back to one of three causes: insufficient or uneven gum application, moisture or humidity exposure weakening the seal after packing, or physical stress during shipping and handling that the seam wasn’t built to withstand.
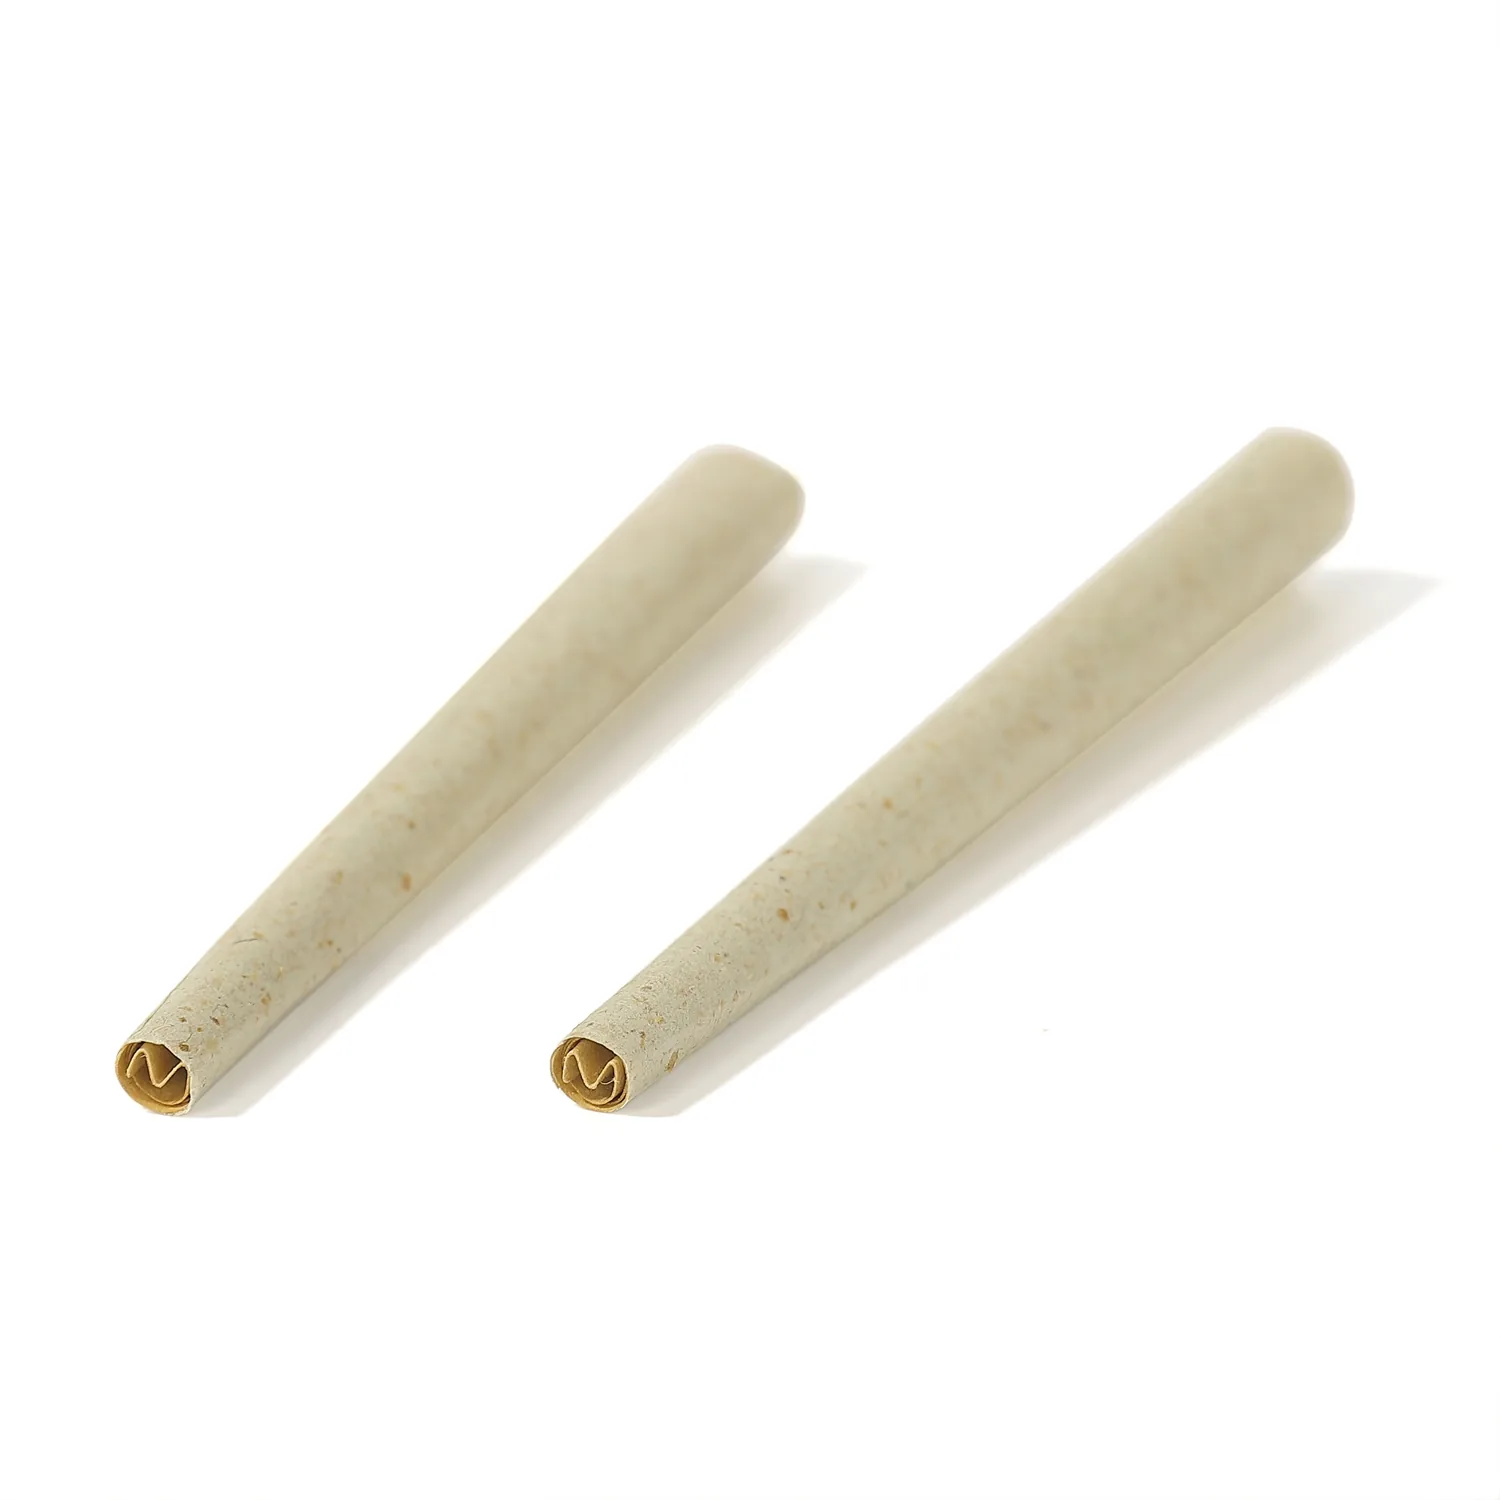
I ask buyers reporting seam problems to tell me exactly when the failure shows up—out of the box, after a few days on a shelf, or only after shipping. That timing is a real diagnostic clue. Immediate failure usually points to the gumming process itself; delayed failure often points to moisture exposure or storage conditions; damage that clusters in certain cartons often points to handling during transit rather than the product itself.
How Do You Visually Inspect for Seam Weakness Before Shipping?
Visual inspection catches more than people expect, if you know what to look for.
A trained inspector checks for visible gum gaps, uneven gum coverage, and any pre-existing seam separation on a sample pulled from each production interval—not just a start-of-run check.
This is the same principle I push on gum application quality generally: a single check at the start of a run doesn’t catch drift that happens partway through, whether from a viscosity shift, equipment wear, or an environmental change in the converting area. I want to see documented interval-based visual inspection, not a one-time check treated as representative of the whole batch.
Documentación de calidad: https://ace-rolling.com/quality-certifications/.
What Sampling Rate Actually Catches Seam Defects Without Slowing Production?
Buyers sometimes assume more sampling always means better quality. It’s really about where you sample.
An AQL-style sampling plan pulled at regular intervals throughout the run catches drift-based defects far more reliably than a larger sample taken only once, because seam issues tend to cluster around specific process moments, not randomly across an entire batch.

I’ve seen buyers request a bigger sample size but only at one point in the run, which misses exactly the kind of gradual drift that causes intermittent seam failures. I’d rather see a modest sample pulled at several points across the run than a large sample pulled once, because the failure mode we’re actually trying to catch is usually a process drift issue, not a uniform batch-wide defect.
| Sampling approach | What it catches |
|---|---|
| Large sample, single point | Uniform batch-wide defects |
| Modest sample, multiple intervals | Process drift and gradual defects |
Does Canoeing Actually Trace Back to the Seam, or Somewhere Else?
This is a genuinely common point of confusion, and it’s worth separating clearly.
Canoeing—uneven burning down one side of the cone—is usually a paper density or rolling technique issue, not a seam issue, but a weak seam can make canoeing worse by letting the cone structure shift during use once the seal starts to give.
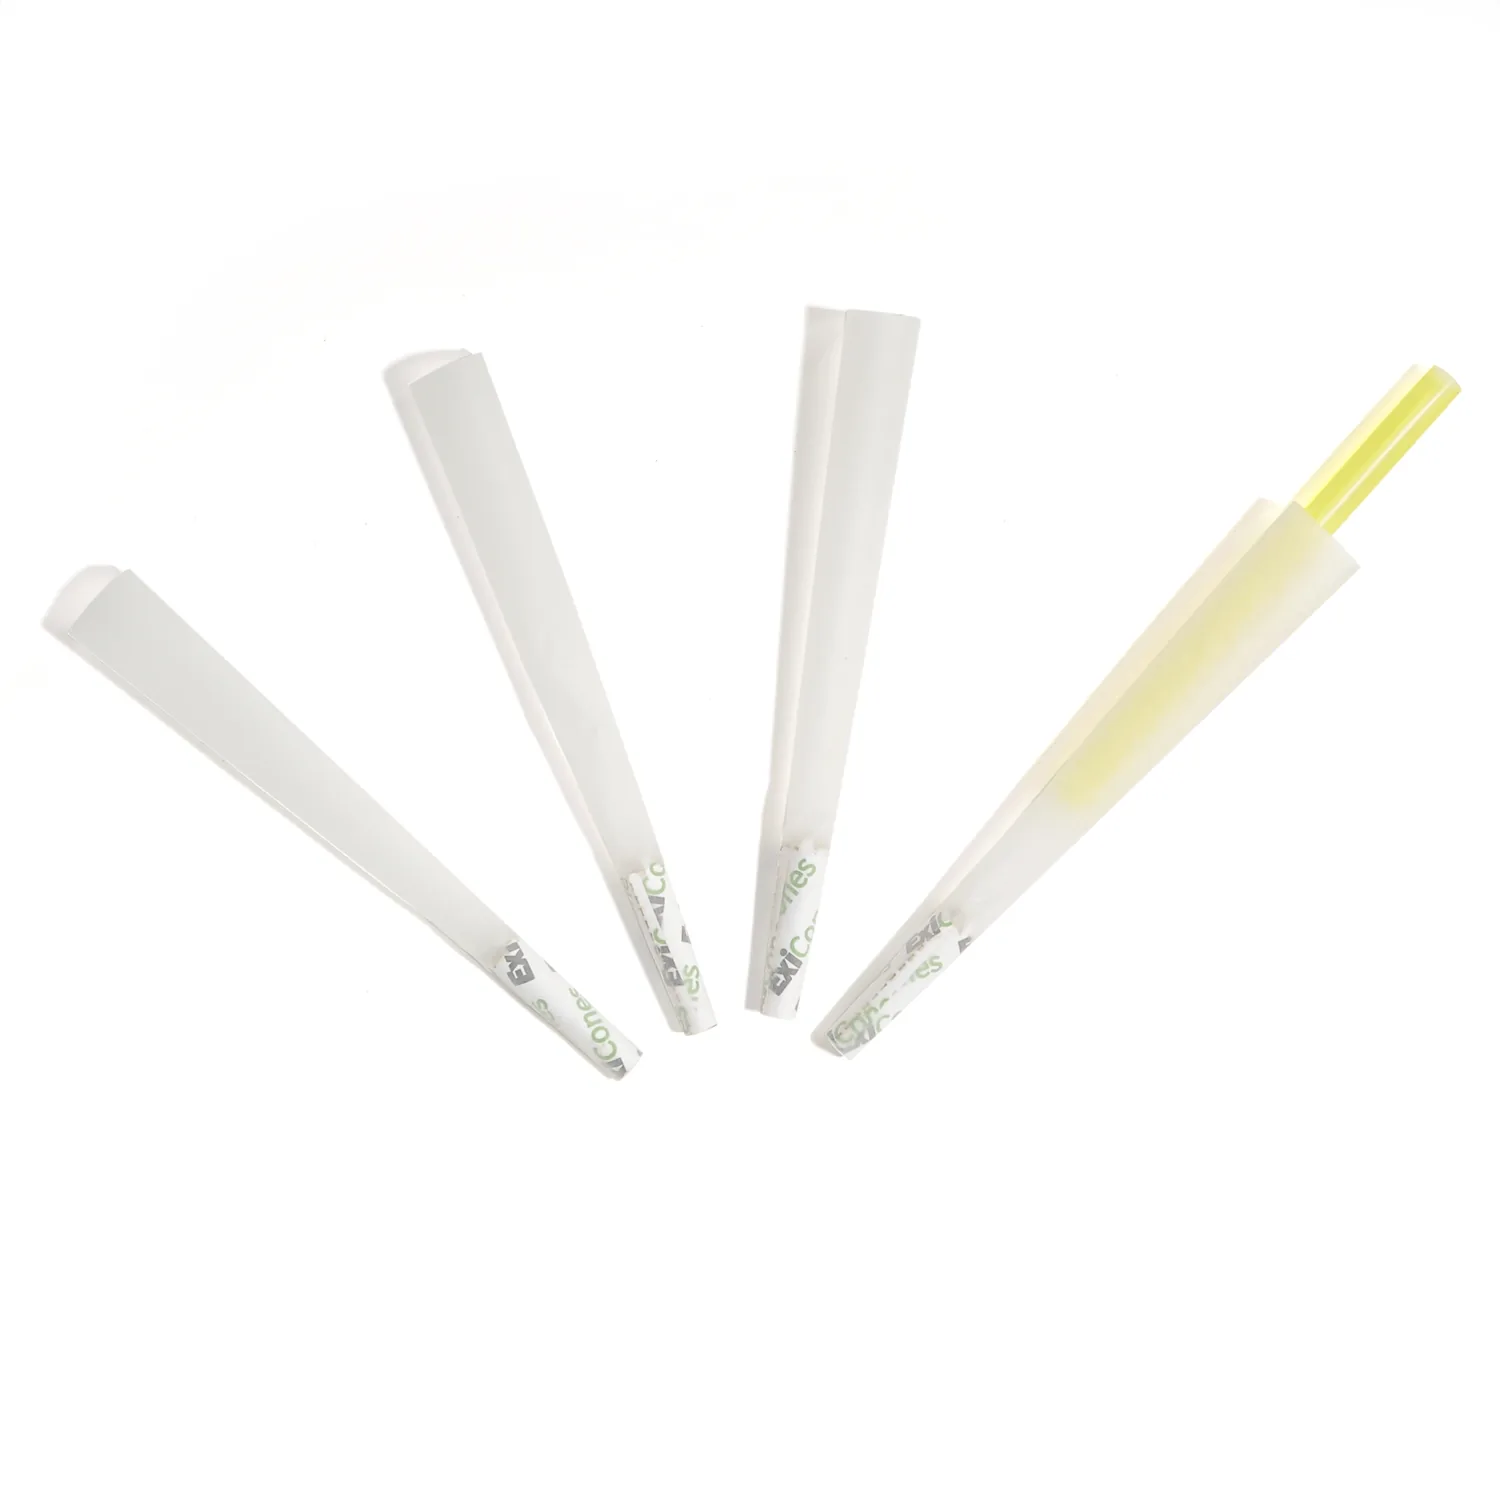
I ask buyers to separate these two complaints when they come in, because they point to different corrective actions. A canoeing complaint with an intact seam points toward paper density or fill packing consistency. A canoeing complaint paired with visible seam separation points toward the seam itself contributing to the structural failure, which changes where I’d focus the QC review.
How Do You Test Seam Strength Under Real Handling Conditions?
A seam that holds on a lab bench doesn’t always hold in a shipping carton.
Run a handling simulation on a full sample carton—actual transit orientation, stacking, and duration—rather than testing individual cones in isolation, since real breakage and seam stress often show up only under those combined conditions.
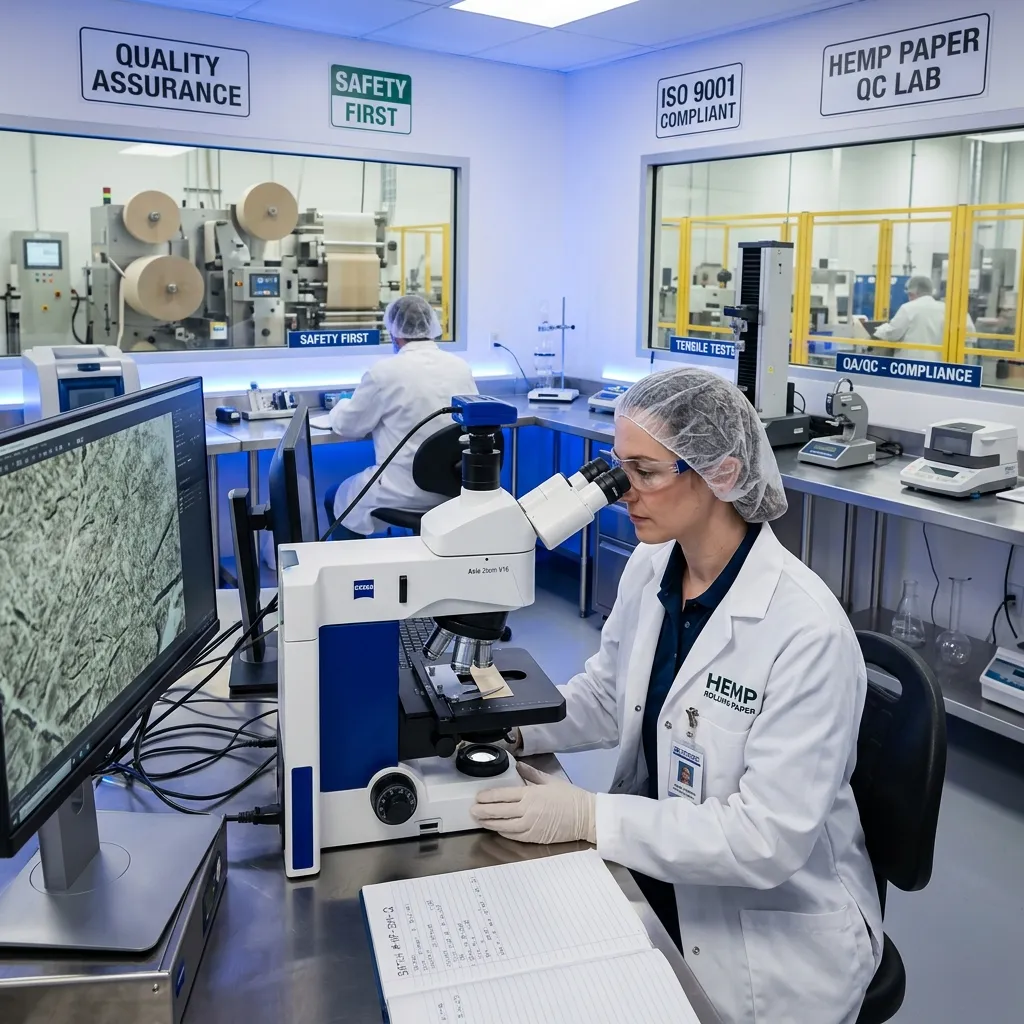
This is the same logic I use for glass tip breakage risk: testing one unit at a time doesn’t replicate what happens when many units are packed together, stacked, and moved through a real freight route. I recommend a full-carton handling test before scaling to a large production order, specifically because seam and structural issues sometimes only appear under that combined real-world stress.
How Do You Set Up a Seam QC Checkpoint With Your Manufacturer?
I’d rather agree on this before the first production run than after a complaint.
Confirm your manufacturer’s visual inspection interval, adhesion testing frequency, and whether they run a full-carton handling simulation—then request documentation from your specific production run, not a generic quality statement.
| QC checkpoint | Qué confirmar |
|---|---|
| Visual inspection interval | Documented, not a single start-of-run check |
| Adhesion testing frequency | Interval-based across the run |
| Handling simulation | Full-carton, not single-unit testing |
| Documentación | Tied to your specific run, not generic |
Preguntas frecuentes
How do you quality-check pre-rolled cone seams?
Check seam integrity at three points: an interval-based visual inspection for gum gaps and coverage, a physical adhesion test throughout the production run rather than only at the start, and a full-carton handling simulation that mimics real shipping conditions. Skipping any one of these three checkpoints lets certain defect patterns slip through undetected.
What usually causes a pre-rolled cone seam to fail?
Seam failure typically traces back to insufficient or uneven gum application, moisture exposure weakening the seal after packing, or physical stress during shipping that the seam wasn’t built to withstand. The timing of the failure—immediate, delayed, or clustered in certain cartons—is a useful clue for narrowing down which cause applies.
Is canoeing the same problem as seam failure?
Not usually. Canoeing, the uneven burn down one side of a cone, is typically a paper density or rolling technique issue rather than a seam problem, though a weak seam can make canoeing worse by letting the cone structure shift once the seal starts to give. Separating these two complaints helps identify the correct corrective action.
Why does sampling at multiple points in a production run matter more than one big sample?
Seam defects often result from process drift—a gradual shift in gum viscosity, equipment wear, or environmental conditions—rather than a uniform batch-wide issue. A modest sample pulled at several points across the run catches this kind of drift far more reliably than a larger sample taken only once at a single point in production.
Does testing individual cones tell you enough about seam strength?
Not fully. Individual cone testing can miss stress patterns that only appear when many units are packed, stacked, and moved together through real shipping and handling. A full-carton handling simulation under actual transit conditions gives a more reliable picture of real-world seam performance than testing single units in isolation.
What should I ask Ace Rolling about seam QC before placing an order?
Ask about visual inspection interval, adhesion testing frequency across the production run, and whether a full-carton handling simulation is part of the QC process. Ace Rolling maintains an ISO 9001:2015 management framework and can walk buyers through documentation for their specific production run before mass production begins.
Ready to Confirm Seam QC Before Your Next Order?
Ask about inspection intervals and handling simulation before you commit to a production MOQ.
- Calidad y certificaciones: https://ace-rolling.com/quality-certifications/
- Pre-rolled cones: https://ace-rolling.com/pre-rolled-cones/
- Cotización: https://ace-rolling.com/contact/