
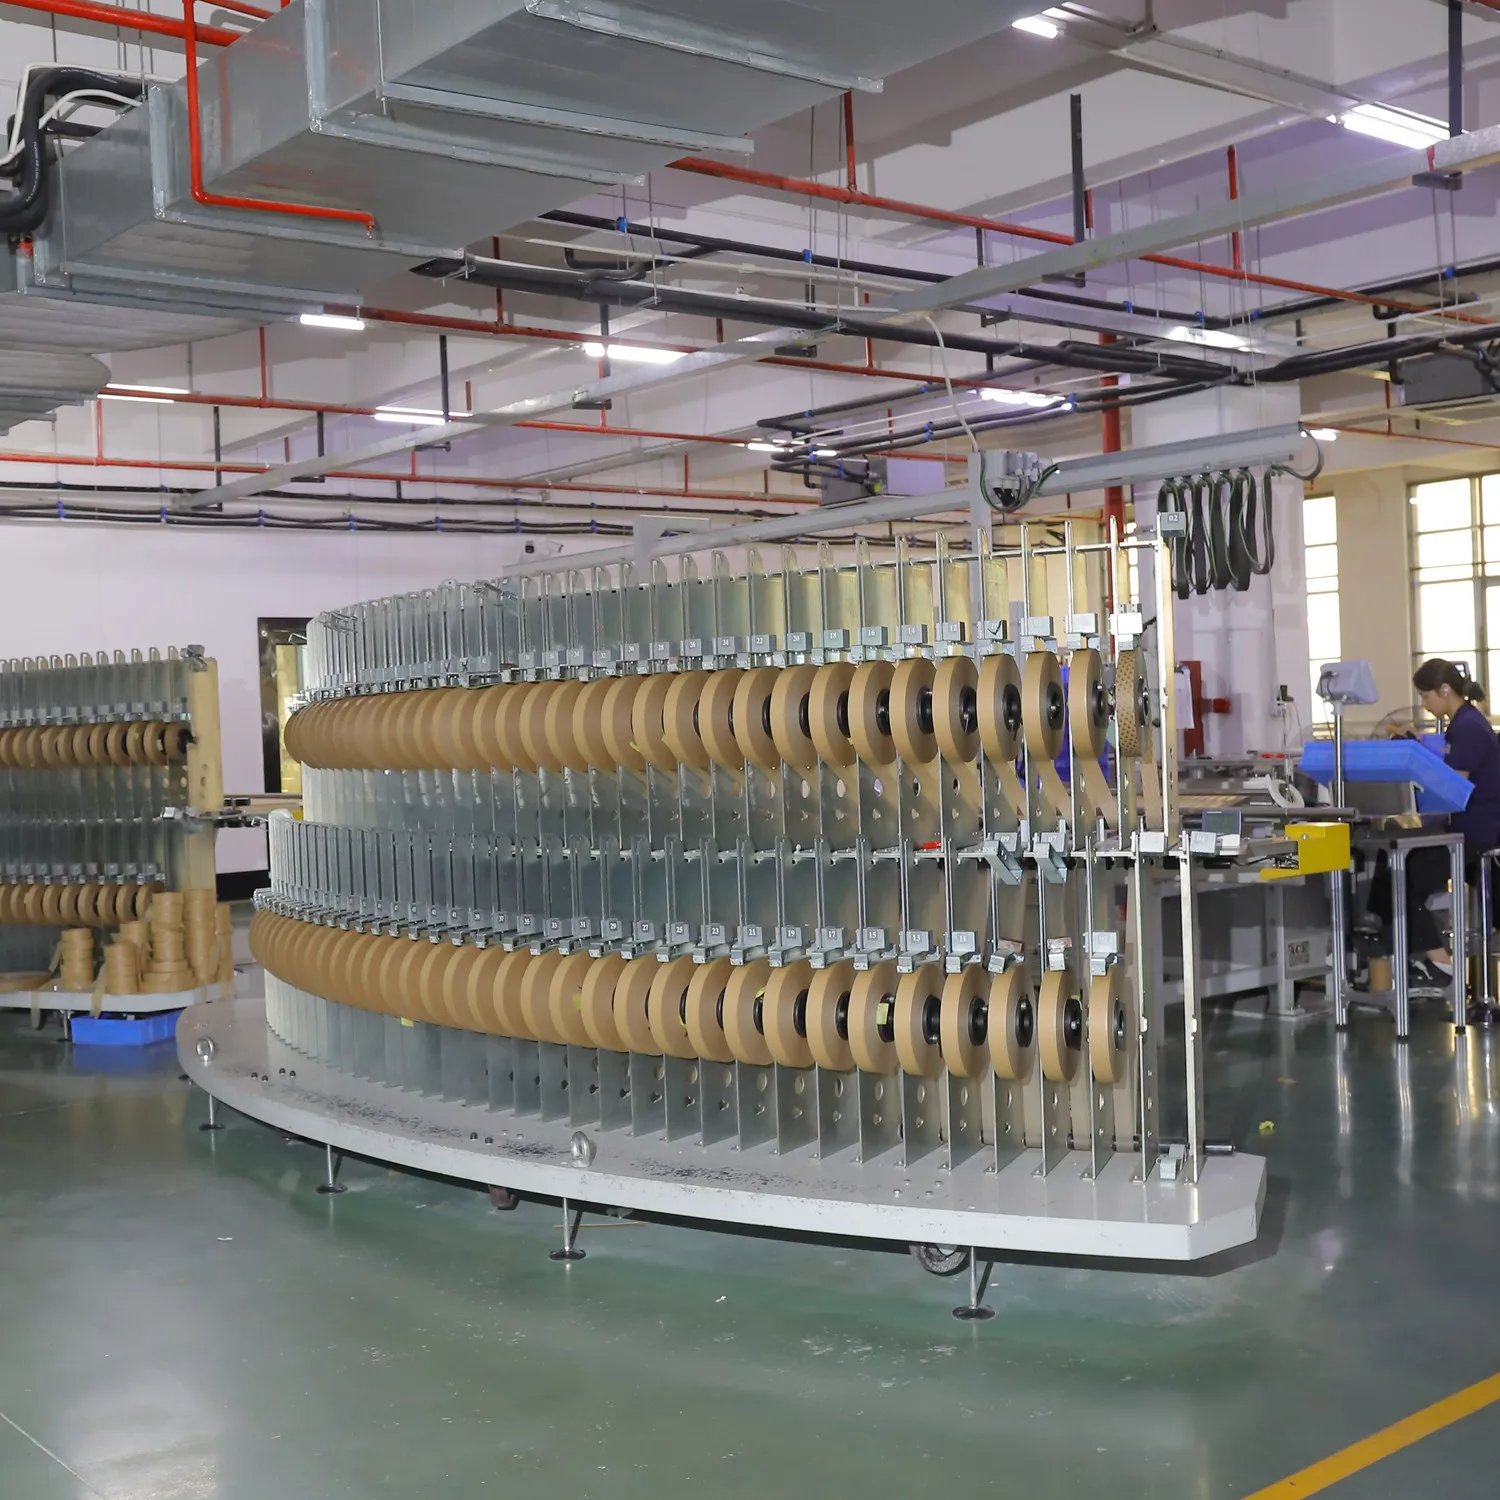
For commercial pre-roll processors and packaging facilities, operating high-speed automated filling machinery requires paper supplies that can withstand continuous mechanical stress. When using vibration-based packing tables, choosing paper cones with inadequate physical properties leads to split seams, crumpled tips, and machine jams.
To optimize production line efficiency, brands must source Knockbox pre-roll cones MD/CD tensile strength parameters that comply with rigorous ISO paper testing standards. Sourcing cones engineered with a balanced Machine Direction (MD) and Cross Direction (CD) tensile ratio ensures that the paper sheets can absorb high-frequency vibrations without tearing, keeping production line defect rates under 0.01%.
Understanding the mechanics of vibration-based filling, ISO 1924 tensile testing standards, and paper fiber alignment technologies will help you audit suppliers and protect your manufacturing margins.
—
How does automated filling impact pre-rolled cone structural integrity?
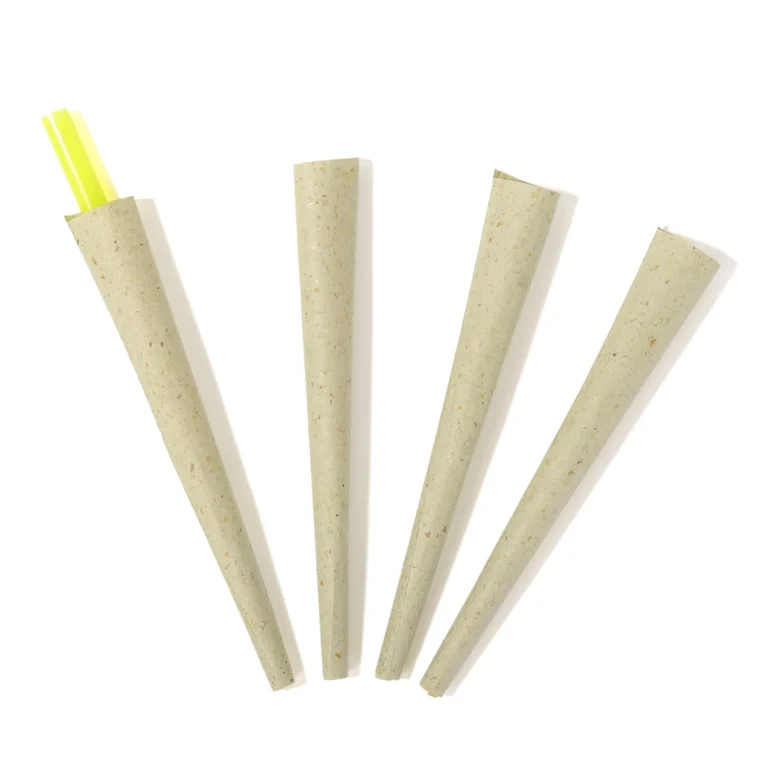
Industrial packing machines, such as the Futurola Knockbox series (including Knockbox 100, 300, and 500 models), process multiple cone sizes concurrently. These include standard 1 1/4 size (84mm length with a 26mm tip), 98 Special (98mm/26mm), and King Size (109mm/21mm or 109mm/26mm).
During the 60-to-90-second packing cycle, the machine subjects the paper cones to rapid vertical oscillations. This physical force consolidates the herbal material inside the cone, eliminating air pockets:
- Vertical Impact Stress: The downward force of the herb column exerts axial pressure along the length of the cone, testing the stiffness of the paperboard tip.
- Radial Expansion Tension: As the material compacts, it exerts outward radial force against the paper wall. This radial expansion puts direct tension on the paper’s glue line and seams.
- Vibrational Fatigue: High-frequency vibrations test the micro-bonding structure of the plant fibers, making weak paper prone to sudden tears.
—
What do ISO 1924 standards reveal about paper tensile parameters?
In paper engineering, tensile strength is measured using the ISO 1924-1 and ISO 1924-2 standards, which define the force required to break a paper strip of a specific width under a constant rate of elongation.
For specialty thin papers (12 GSM to 20 GSM) used in pre-roll manufacturing, the directional alignment of the paper fibers determines its mechanical behavior:
- Machine Direction (MD) Tensile Strength: The strength along the direction the paper web moved on the paper-making machine. For machine-ready bobbins, MD tensile strength should exceed 1.5 kN/m (and up to 1.9 kN/m for high-volume lines).
- Cross Direction (CD) Tensile Strength: The strength perpendicular to the machine flow. Because paper fibers naturally align longitudinally, CD strength is typically lower.
- The MD/CD Ratio: Standard papers have an MD/CD ratio of 2:1 or 3:1. However, since automated filling exerts radial (CD) expansion forces, a high MD/CD anisotropy leads to splitting along the longitudinal seams.
| Paper Material | Base GSM Weight | Required MD Tensile | Required CD Tensile | Target MD/CD Ratio |
|---|---|---|---|---|
| High-Tensile Rice | 12 GSM – 13 GSM | ≥ 1.5 kN/m | ≥ 0.9 kN/m | 1.6 : 1 |
| Органическая конопля | 13 GSM – 14 GSM | ≥ 1.6 kN/m | ≥ 1.0 kN/m | 1.6 : 1 |
| Refined Wood Pulp | 14 GSM – 18 GSM | ≥ 1.8 kN/m | ≥ 1.1 kN/m | 1.5 : 1 |
—
How do advanced paper-making processes optimize the MD/CD ratio?
To prevent splitting on the Knockbox table, direct manufacturers utilize advanced headbox (流浆箱) and slice geometry control to randomize fiber orientation during the wet-end forming phase.
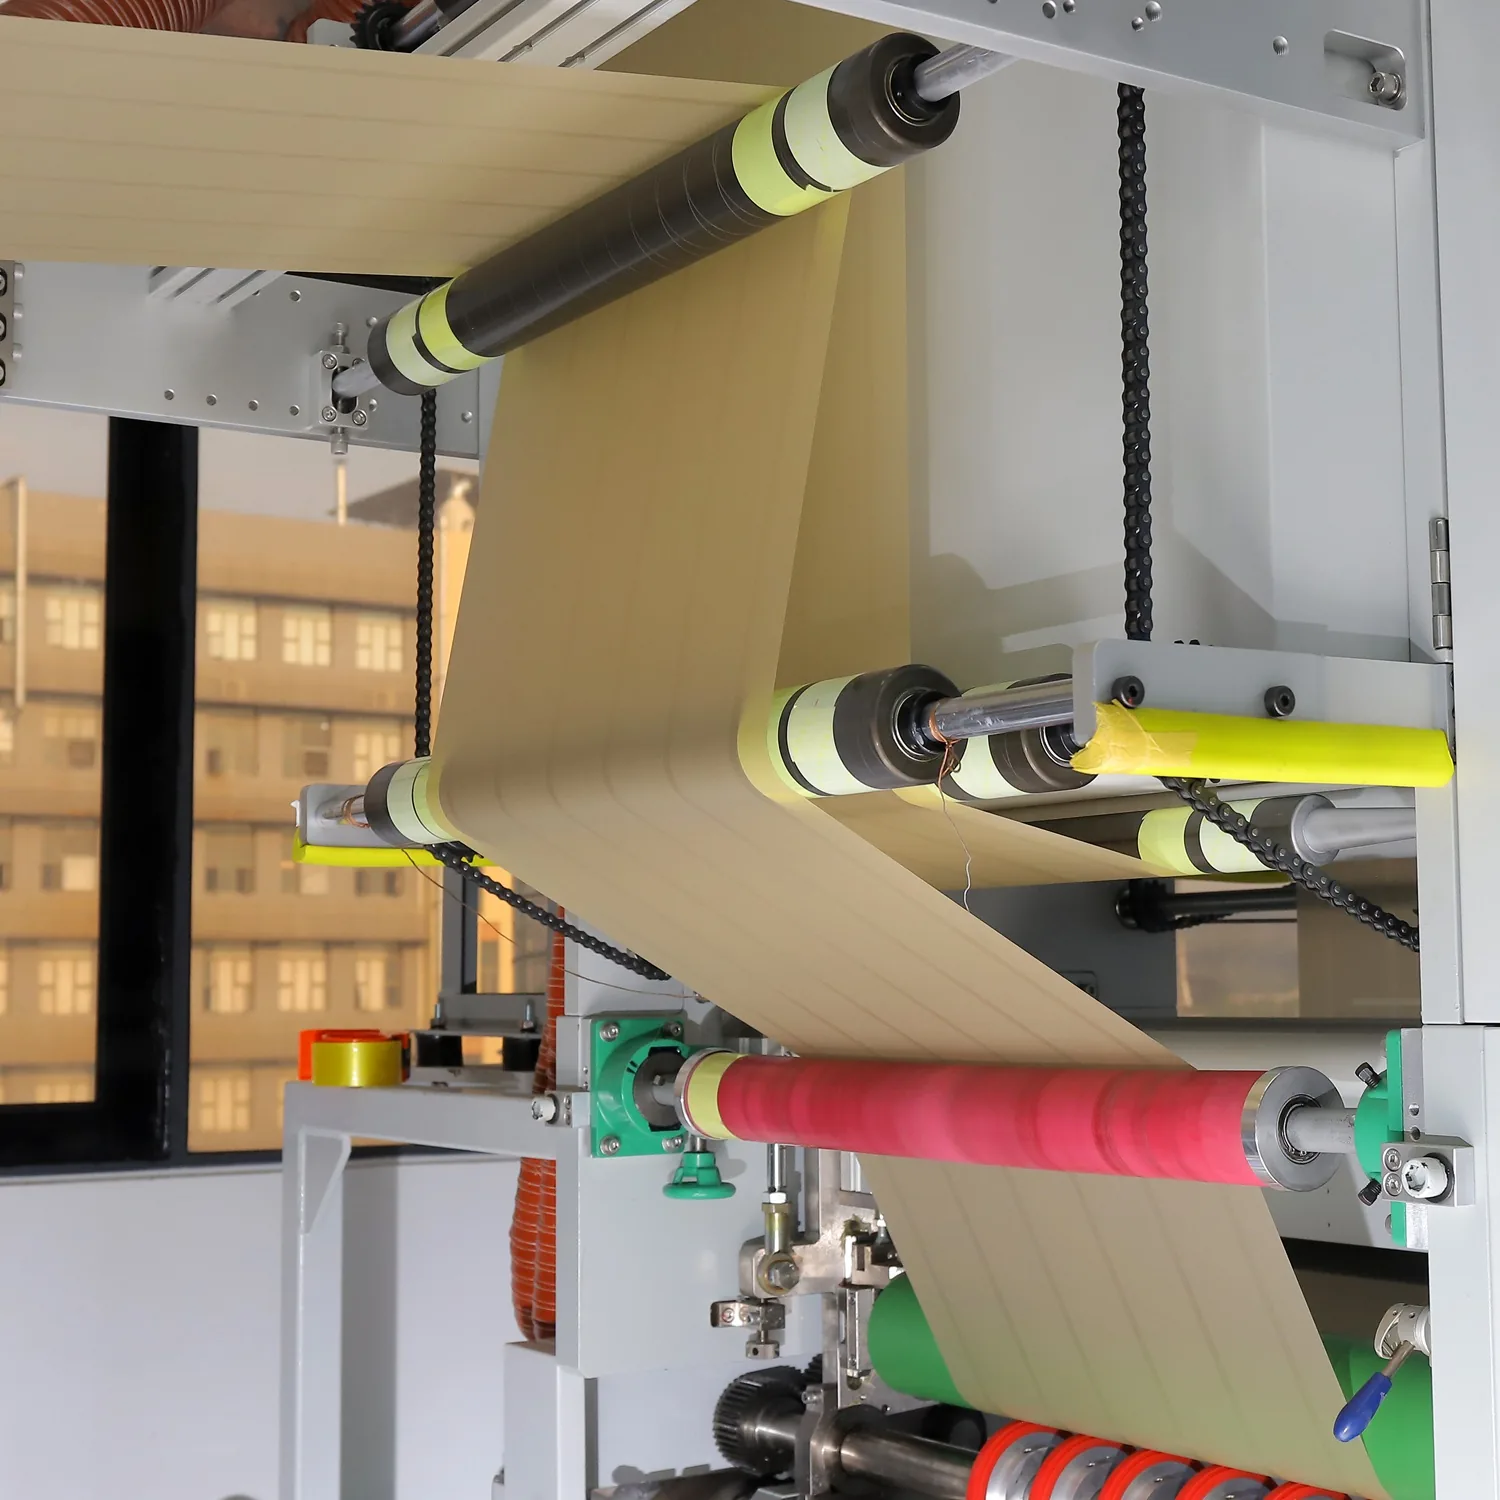
Наше производственное предприятие оптимизирует технологичность бумаги за счет:
- Управление турбулентностью: Создание контролируемой микротурбулентности в напорной камере для предотвращения группировки волокон и их выравнивания исключительно в машинном направлении.
- Регулировка скорости струи к сетке: Согласование скорости струи суспензии со скоростью сетки для случайного распределения волокон, приближая соотношение MD/CD к сбалансированной конфигурации 1,5:1.
- Точная резка: Использование высокоточных круглых лезвий для чистого разрезания рулонов бумаги без образования микроразрывов по краям, которые могли бы стать точками концентрации напряжения при намотке.
Контрольный список поставок для автоматического наполнения предварительно скрученных изделий
- [ ] Убедитесь, что ваши предварительно скрученные конусы совместимы с конкретными формами лотков вашей модели Knockbox.
- [ ] Запросите листы испытаний на растяжение по ISO 1924 (с указанием значений MD и CD) из заводской лаборатории.
- [ ] Убедитесь, что листы бумаги имеют соотношение анизотропии MD/CD 1,6:1 или ниже.
- [ ] Протестируйте пробную партию из 1000 конусов на полной скорости упаковки машины, чтобы подтвердить уровень расслоения ниже 0,01%.